One Integrated CDMO Model
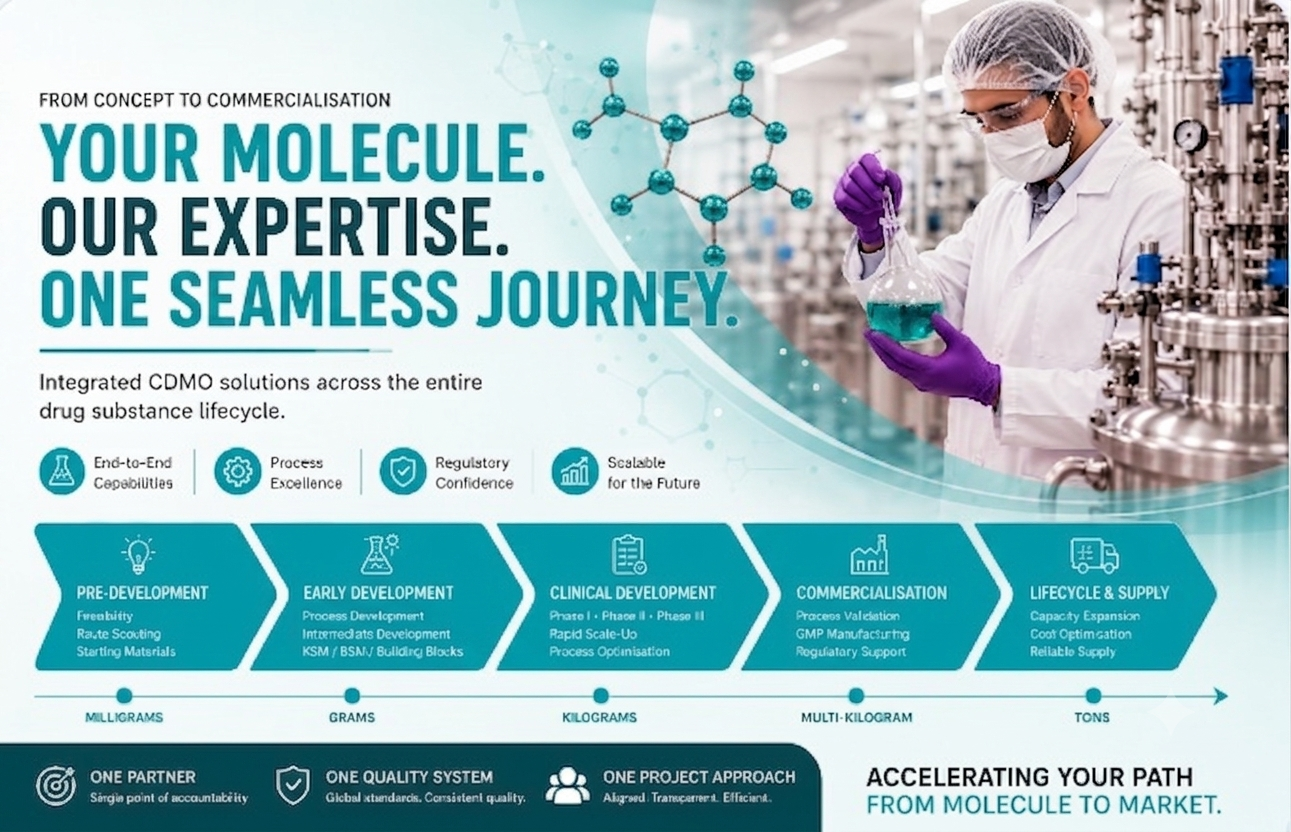
From KSMs to Commercial APIs — One Quality System, One Integrated Delivery Model.
Three complementary businesses — Glochem, Chieron and Maksons — operate as one integrated CDMO platform with a dedicated R&D centre and dedicated manufacturing plant. Built on strong chemistry know-how, advanced reaction capabilities, robust project management, and complete transparency with seamless information flow for partners.
One platform, three strengths: Glochem, Chieron and Maksons in a single backward-integrated CDMO platform
Our Vision — Build one of the most successful, chemically innovative and science-driven platforms in the industry
Three complementary businesses, one integrated platform — Enabling fast-track intermediate & API development, efficient manufacturing and reliable supply across regulated global markets. Three complementary companies, one quality system and one project management office.
Glochem Industries
Established 1995 · Hyderabad, TG
- 25+ years of experience in manufacturing API for regulated markets (US, EU, JP & Korea)
- Global API leadership in CVS and Anti-histamines
- USFDA, EU-GMP, TGA, PMDA, KFDA, WHO, ANVISA approved (USFDA last audited in Nov 2024)
- Serves 50+ countries across regulated markets
Chieron Active Ingredients
Established 2007 · Nellore, AP
- Serving API & adv. intermediate to US, EU, JP & Korea markets for generic & CDMO players
- Leadership in 15 to 20 APIs through continuous manufacturing in CVS, Anti-diabetic and CNS
- USFDA Approved — Last audited in June 2026 with zero observations
- ~320 KL capacity; USFDA, EDQM, PMDA, KFDA approved
Maksons Finechem
Established 1988 · Ankleshwar, GJ
- Serving intermediates and advance intermediates to originators & innovators
- Extends backward integration into raw materials and KSM
- Strengthens cost competitiveness and supply reliability
Integrated as one group, delivering end-to-end CDMO solutions from KSMs through to commercial APIs
One group, three heritages
Glochem Industries (1995), Chieron Active Ingredients (2007) and Maksons Finechem (1988) operate as a single platform, with dedicated cGMP and non-GMP facilities for Performance & Speciality Chemicals, KSMs, advanced intermediates and APIs.
Accredited across major markets
Sites accredited to USFDA, EU-GMP, WHO-GMP, ISO 9001, ISO 14001, ISO 45001 and PSCI. Sustainability performance independently recognized through EcoVadis Gold, CDP and SBTi. Targeting EcoVadis Platinum for U1, U2 by Dec'27.
Innovation ecosystem for speed
Integrated R&D centers in Ahmedabad and Hyderabad, three plant-based process development centers and a dedicated pilot plant at Chieron enable rapid optimization, technology transfer and scale-up from lab research to commercial manufacture.
GMP & non-GMP under one roof
Glochem and Chieron manufacture KSMs, advanced intermediates and APIs under cGMP from USFDA, EDQM and PMDA-approved sites. Maksons adds non-GMP development and manufacture from process development to commercial supply.
Where we are heading (Expansion Roadmap)
Entering high-value oncology and peptide segments in Q3'26 through established CMO partnerships, commercially operational for global supply.
R&D centre in Dec 2025 & new CDMO R&D centre based out of Hyderabad, commencing operations by Oct'26 for process development, tech transfer and scale-up.
CDMO R&D centers planned in Princeton, New Jersey and Seoul, South Korea in 2027.
Q3 established CDMO partnerships updated for October 2026
Established across regulated markets, with a deep filing base and matching chemical engineering competencies
USDMF 21
& 15 undergoing
15 CEP
& 10 undergoing
4 JDMF
& 0 under filing
9 KDMF
& 10 under filing
Add Details
Add Details
REGULATED MARKETS SERVED
United States, Japan, South Korea, Brazil, UK, Germany, Switzerland, Belgium, Italy, Canada, Poland, Czech Republic, Australia, China, Austria.
Approvals Held
Core chemical engineering competencies
- Process development and optimisation: Route design focused on yield, purity and scalability
- Scale-up expertise: Seamless lab to pilot to commercial transition
- Process engineering: Resolving scale-up and operational challenges
- Process safety and risk management: Calorimetry, hazard evaluation and safe process design
- Impurity control: Consistent quality and regulatory compliance
- Robustness and reproducibility: Controlled parameters, batch-to-batch consistency
Three engagement models, shaped around where your molecule is and how you want to share risk
Tailored collaboration frameworks de-risk development, secure intellectual property and accelerate commercial supply.
Joint development JDA
Best when you want to co-invest and share upside
IP: Shared ownership
COMMERCIAL: Risk and reward shared
EXECUTION: Milestone-based, R&D to launch
FIT: Novel routes needing joint invention
Technology Licensing
Best when you want a proven route fast
IP: Licensed to Customer
COMMERCIAL: Exclusive, semi- or non-exclusive
EXECUTION: Full tech transfer with documentation
FIT: Rapid market entry on known chemistry
CDMO and CMO Contract Manufacture
Best when you want capacity and reliability
IP: IP belongs to customer
COMMERCIAL: FTE (Full-Time Equivalent) & FFS (Fee-for-Service)
EXECUTION: Lab through to commercial supply
FIT: Scale-up and sustained supply
A hands-on project management office gives you one point of contact and full visibility throughout
Framework: Initiation → Planning → Execution → Monitoring → Closure
- End-to-end approach: Dedicated project managers and a single point of contact | Cross-functional coordination across R&D, manufacturing and regulatory.
- Structured lifecycle framework: Initiation through planning, execution and monitoring to closure | Milestones, KPIs and active risk management.
- Technology and transparency: Real-time dashboards and progress tracking | Weekly or fortnightly updates by email or teleconference | Regulatory-ready documentation throughout.
- Proven track record: On-time delivery against committed milestones | Flexible engagement through collaboration or partnership.
- Value for innovators and CDMOs: Accelerated time to market | Full visibility and scalable operations | Smooth regulatory filings.
A security and compliance framework built so innovators can share their chemistry with confidence
Your IP stays yours: customer-owned rights, role-based access and full audit trails, backed by a QMS that is audit-ready for the US, EU and Japan.
- IP protection: IP rights fully retained by the customer | Strong confidentiality agreements and data safeguards | Controlled access and secure handling of customer-specific information.
- Data protection and privacy: Strong IP protection and confidentiality controls | Role-based access, encryption and audit trails.
- Regulatory and quality compliance: ICH Q7 and Q11 compliant, cGMP operations | Robust QMS covering CAPA, change control and deviations | Audit-ready for US, EU and Japan markets.
- Risk management and EHS: HAZOP-based risk assessments | Expertise in hazardous and complex chemistries | Strong EHS and business continuity systems.
- Customer assurance: Full traceability and data integrity | Reliable partner for regulated global markets.
Three phases from enquiry to supply, explicit service commitments at every step
48 to 96 h
Response time to a new enquiry
> 98%
Quality standards achieved
QUOTIF
Quality, On Time, In Full
1 Initial phase (Setting the stage for success)
- Client enquiry and initial communication - quick, responsive engagement to understand your requirements
- Onboarding and documentation - seamless integration of project details and regulatory needs
- Feasibility assessment and literature review - data-driven evaluation to ensure optimal project planning
2 Development phase (Process innovation)
- Optimized synthesis route design - efficient, cost-effective pathways tailored to your project
- Advanced laboratory development and testing - robust, reproducible processes for seamless scale-up
- Strategic raw material sourcing and evaluation - high-quality inputs for consistent product performance
3 Execution phase (Delivery and support excellence)
- Proposal submission and approval - transparent planning and clear timelines for smooth execution
- Procurement and timeline commitment - materials and resources in place for on-time delivery
- Product delivery and ongoing support - reliable handover with continuous collaboration and support
Backward-integrated manufacturing across three sites delivers ~435 KL of installed capacity
Three manufacturing sites across three states, each with strong port and air connectivity — and a presence in established pharma hubs like Hyderabad and Gujarat provides ready access to CMO partners when needed.
Three State-of-the-Art Manufacturing Sites
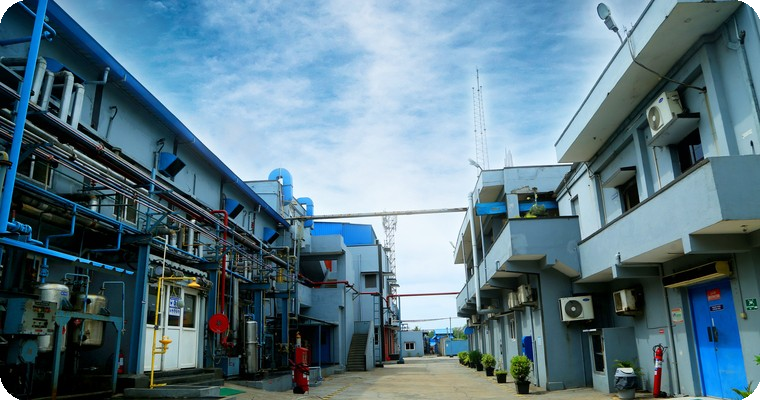
Glochem · Hyderabad
96.7 KL Capacity across 5 blocks | USFDA, EU-GMP, TGA, PMDA, KFDA Approved
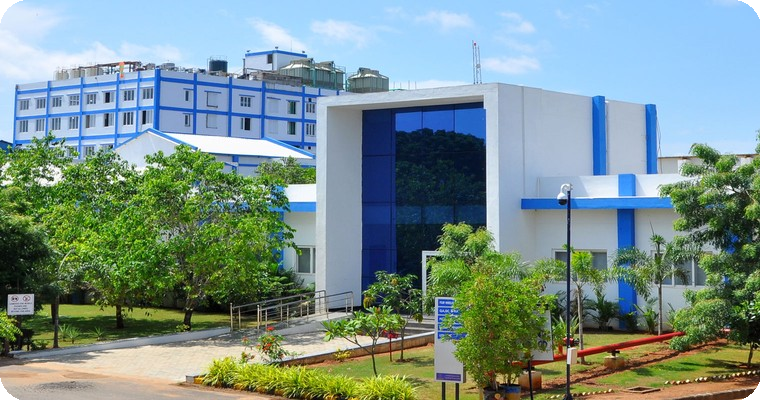
Chieron · Nellore
~316.2 KL Installed Capacity (+200 KL underway) | USFDA, EDQM, PMDA, KFDA Approved
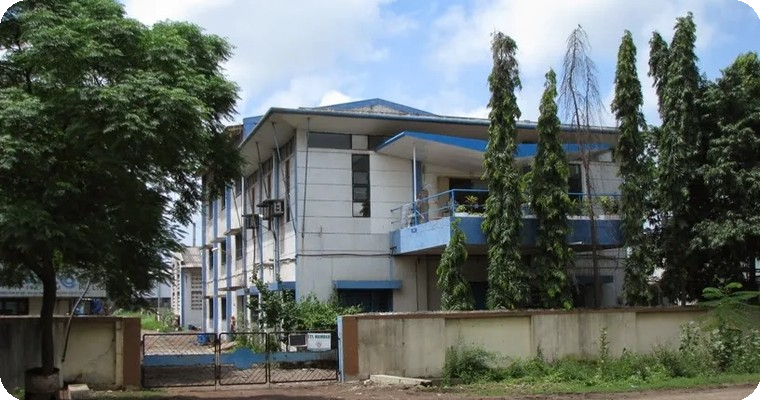
Maksons · Ankleshwar
20.1 KL Installed (+150 KL underway) | Dedicated Non-GMP CDMO Site
Backward-integrated manufacturing across three sites delivers ~435 KL of installed capacity
| Site / Established | Reactors | Capacity | Value Chain | Capabilities | Top Molecules |
|---|---|---|---|---|---|
| Glochem (1995) | 46 (incl. 8 glass-lined); Capacity per reactor ranges from 0.5 to 6.3 KL | 96.7 KL across 5 blocks | API manufacturing (cGMP) | Pyridine Synthesis (heterocycle construction), Deprotection (selectivity-dependent) | Cetirizine, Amlodipine, S-Amlodipine, Phthalimido-Amlodipine |
| Chieron (2007) | 60 (SS, GLR, pressure); Capacity per reactor ranges from 0.5 to 10 KL | ~316.2 KL + 200 KL underway | API manufacturing (niche global leadership), CDMO | Nitration, Grignard Reaction, Protection/Deprotection, Imidazole Synthesis | Olmesartan, Lacosamide, Levetiracetam, Tetracaine Base |
| Maksons (1988) | 13 (incl. 3 glass-lined); Capacity per reactor ranges from 0.25 to 2 KL | 20.1 KL + 90-150 KL underway | KSM, intermediates & Performance & Speciality Chemicals | Diazotization, N-Bu-Li handling, Cryogenic Reaction at -20 °C, Chlorosulphonation | BromoSynchem, MNIDE & Dimol |
Platform Scale & Expansion Plans
~435 KL
Installed Reactor Capacity
(300-350 KL underway)
~120 Reactors
Across Three Manufacturing Sites
Glochem · Chieron · Maksons
35+ Yrs
Manufacturing Heritage
Across the Integrated Platform
Expansion Plans for Next 1 Year
Entering high-value oncology and peptide segments in Q3 2026 through established CMO partnerships.
- Augment CDMO strength to support internal manufacturing and strengthen the molecule portfolio
- Expand API capabilities, portfolio and capacity
Two additional acquisitions planned, adding 650 - 1,000 KL of capacity by end-March 2027
Maksons Finechem: a dedicated non-GMP CDMO site taking programmes from gram scale to commercial tonnage
1988
Established
35+ years of expertise
~50%
Output exported
to regulated & semi-regulated markets
250L–2,000L
Multipurpose GLR and SSR
reactor range
+150 KL
Additional capacity by end 2027
civil work complete
Integrated service
Process development, scale-up and commercial manufacturing on one site
Equipment
Glass-lined and stainless steel reactors, centrifuges, RVDs and FBDs
Utilities
-20 °C chilling, high vacuum and thermic fluid heating to 300 °C
Quality systems
Process validation, analytical method development and validation, equipped QC labs
Partnership
Confidentiality, supply chain security and consistent product quality
Unit-level manufacturing capability | Capacity, consents, reactors and clean rooms at a glance
| Parameter | UOM | Unit 2 - Glochem USFDA approved | Unit 1 - Chieron USFDA approved | Unit 3 - Maksons Non-GMP |
|---|---|---|---|---|
| Installed capacity | KL | 96.70 | 316.16 | 20.13 |
| CFO water consent | KLD | HTDS 53.7 · LTDS 15.5 | HTDS 35 · LTDS 61.8 | CETP 13 |
| Water utilisation vs consent | % | HTDS 33.4 KLD, 62% · LTDS 4.0 KLD, 25% | HTDS 8 KLD, 23% · LTDS 27 KLD, 44% | 11 KLD, 84% |
| CFO product mix consent | MT / month | 25.3 | 41.66 | 3.0, applied for 29.3 subject to CTO approval |
| Production vs consent | MT / month | 18.0 | 9.61 | 2.1, applied for 3.0 subject to CTO approval |
| Reactors - glass-lined | Nos | 8 | 21 | 3 |
| Reactors - stainless steel | Nos | 38 | 38 | 10 |
| Reactors - pressure | Nos | 0 | 1 | 0 |
| Working volume range | KL | 0.5 to 6.3 | 0.5 to 10 | 0.25 to 2 |
| Production blocks | Nos | 5 intermediate blocks plus 3 pharma blocks | 2 production blocks with clean rooms plus 1 pilot plant | 1 intermediate block, new block from Dec 2026 adding ~150 KL |
| Clean rooms | Nos | 3 | 7 | 0 |
| Powder processing areas | Nos | 2 | 8 | 0 |
HTDS = high total dissolved solids; LTDS = low total dissolved solids; CETP = common effluent treatment plant; CFO = consent for operation; CTO = consent to operate
Each unit brings a distinct reaction toolkit, together covering the transformations innovator requirement
A science-driven R&D engine of 226+ scientists, integrated with manufacturing
226+
Scientists supporting complex chemistry programs
55+
PhDs across the R&D organisation
91+
Fume hoods across labs
9 Labs
(5 owned + 4 partnered)
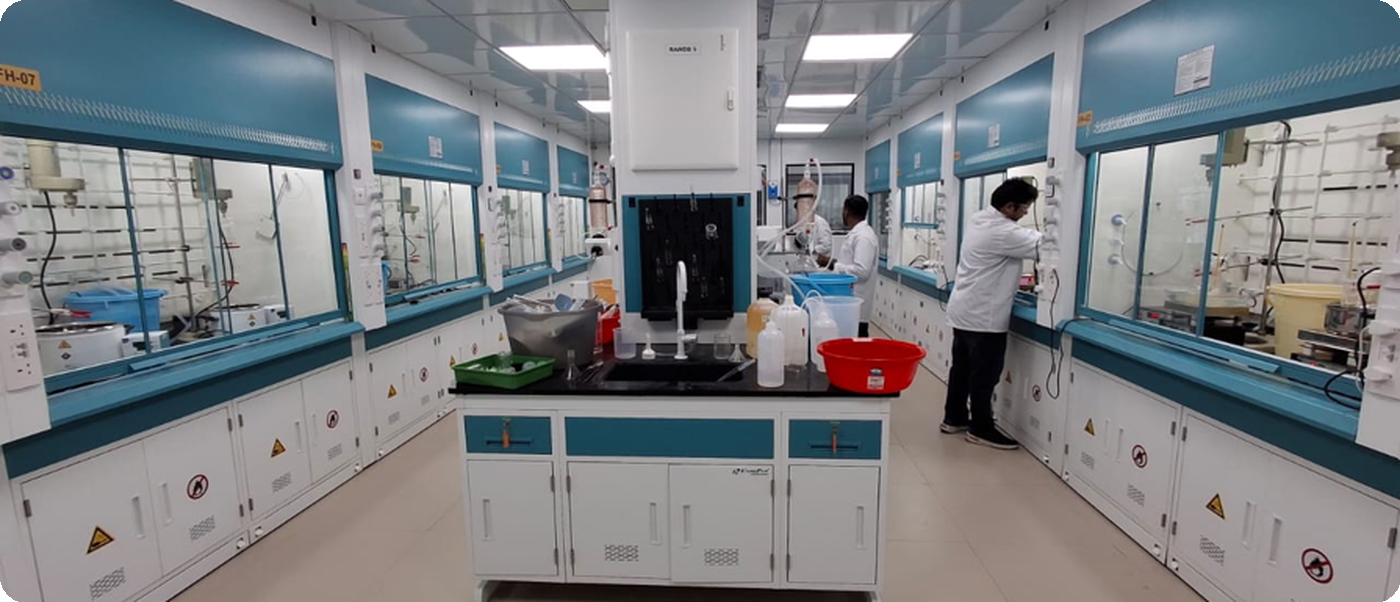
Process Development & Synthesis Lab
91+ Fume Hoods with Advanced Reaction Control Systems
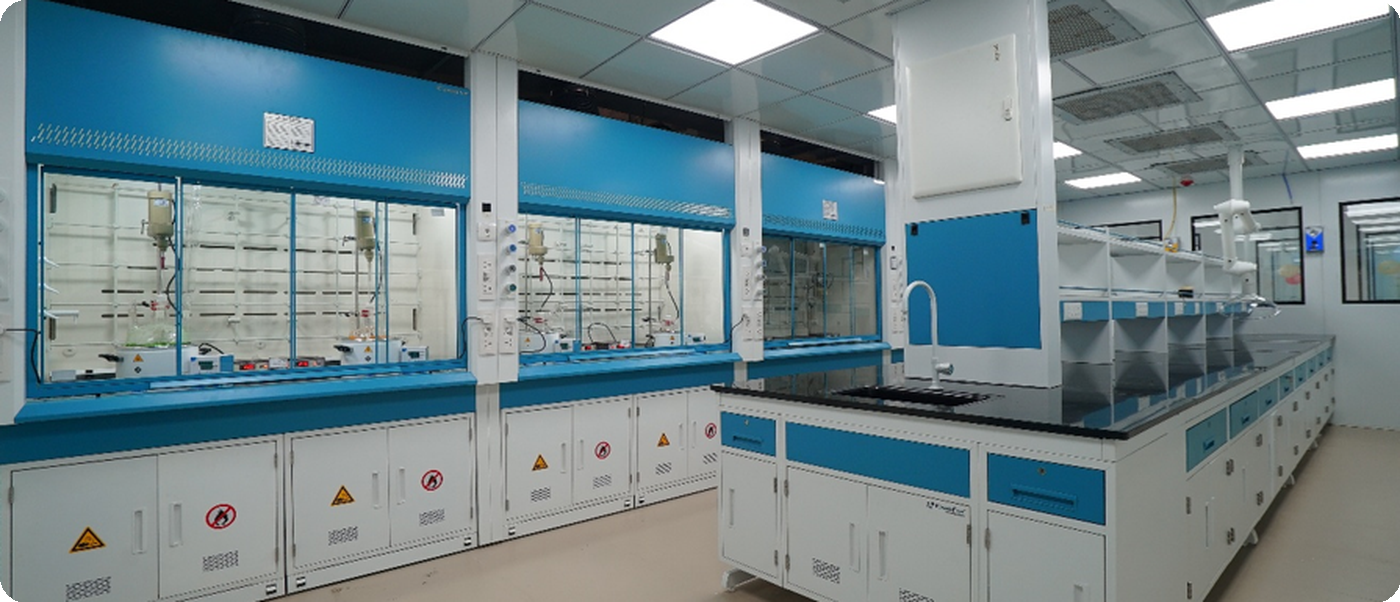
Analytical Instrumentation Suite
HPLC-MS-MS, GC-MS, XRPD, TGA & NMR Infrastructure
Analytical capability covering the full CMC toolkit, phase-appropriate and aligned to ICH expectations
Chromatography
Spectroscopy
Physical and Thermal Assessment
Stability and Degradation
Chromatography
Spectroscopy
NMR
Trace Analysis
Physical, Thermal and Stability
A structured six-stage process development approach
Alignment with customer requirement
Define purity, impurity profile, yield and scale | Align on regulatory expectations (ICH or customer) | Ensure full documentation and traceability
Route design and feasibility
Route scouting and selection | Benchmark against literature, prior art and technical package | Validate yield, purity, cost & ensure safety
Process development & optimization
Finalize reagents and solvents | Optimize reaction parameters like temperature, pressure and cycle time | Design for robustness and scalability
Process safety
Reaction calorimetry to evaluate exothermicity, and gas evaluation | DSC for thermal decomposition | Define safe operating limits and mitigation strategies
Process Engineering & Pre-Scale-up studies
Scale-down experiments | Process engineering studies | Laboratory demonstration / validation | Readiness for plant-scale validation
Environmental assessment
Evaluate effluent streams, solvent usage and waste generation | Identify waste minimization and solvent recovery opportunities | Ensure environmental and regulatory compliance
Validation, Scale-Up & Delivery
Analytical Method Development & Validation
- Analytical method optimization - mobile phase, column, gradient, temperature, concentration, diluent, run-time
- Check specificity, precision, accuracy, linearity, range, LOQ, LOD, robustness, solution stability
Plant-Scale Process Validation
- Scale to ≥1 kg and production level
- Confirm consistency & robustness
- Define CQAs & CPPs
- Confirm yield & reproducibility
- Commercial manufacturing readiness
GMP, Stability & Regulatory Support
- GMP & validation documentation
- ICH-compliant stability studies
- Regulatory filing support as required
- CMC & regulatory documentation support
- Data integrity & compliance
Client Alignment
- Submit a complete technical dossier
- Review yield, quality, scalability and risks
- Align on the next phase (scale-up or technology transfer)
Supply Chain Reliability
- Dual sourcing strategy and vendor qualification
- Risk mitigation for raw materials and logistics
- Business continuity planning for uninterrupted supply
Lifecycle Management
- Continuous process monitoring and improvement post scale-up
- Change control and regulatory impact assessment
- Ongoing optimization for cost, quality and sustainability
Safety by design, contamination control by strategy and sustainability by commitment
A long-standing quality, compliance and sustainability track record
| Unit | Sustainability | Quality | Track Record & Culture |
|---|---|---|---|
| Glochem Industries |  🥈 SILVER | Top 15%EcoVadis Sustainability Rating | Audit completed in 2024 | Recognized as a strong employer/culture (independent workplace recognition) |
| Chieron Active Ingredients |  🏆 GOLD | Top 5%EcoVadis Sustainability Rating | Audit completed in 2026 with zero observations | Long-standing (10-15+ year) regulatory track record across multiple agencies - de-risks any new customer qualification |
Safety by design, contamination control by strategy and sustainability by commitment
Environment, health and safety
- Environment: zero liquid discharge, solvent recovery, waste minimisation and green chemistry in route design
- Climate: CDP score of B in 2025 and an SBTi commitment on emissions reduction
- Social: Golden Peacock Award for occupational health and safety, and independent Great Place to Work recognition
- Governance: Transparent ESG oversight and PSCI-aligned responsible supply chain practices
- Certified: ISO 9001, ISO 14001, ISO 27001 and ISO 45001 across the platform
Contamination control strategy
- Dedicated facilities: Cleanroom segregation, dedicated HVAC zones, pressure differentials and airlock systems
- Engineered barriers: Closed system transfers, dynamic HEPA filtration, magnetic line filters and micron polishing
- Process design: Validated cleaning procedures, TOC monitoring, swab and rinse testing for cross-contamination prevention
- Personnel & materials: Strict gowning protocols, unidirectional material flow and personnel decontamination
Quality Assurance & Data Integrity
- Data Integrity: 21 CFR Part 11 compliant systems, audit trails enabled, dual verification protocols
- QMS Architecture: Comprehensive electronic quality management covering deviations, OOS, CAPA and change controls
- Analytical Validation: Method validation per ICH Q2(R1), stability testing per ICH Q1A(R2)
- Global Audits: Successful audit track record with USFDA, EDQM, PMDA and leading innovator pharma clients
Seven engineered control measures keep foreign and ferrous matter out of the product stream
Dynamic filter HEPA, 0.3 µm
Ensures particle-free filtration and transfer operations. Located outside the cleanroom to minimise the risk of particulate contamination inside it.
Magnetic line filter at filtrate receiving line
Prevents the entry of ferrous and iron particles into the cleanroom through the filtrate receiving line.
Micron filters 0.5 µm and 0.2 µm
Provide effective particulate control and ensure particle-free process streams entering and used within the cleanroom.
Electropolished lines with jacket
Minimises product contact friction, avoids metallic particulate shedding, and enables jacketed temperature control during transfer.
Magnetic grilles and traps at sieving
Capture and control ferrous particles generated during the sieving operation and prevent their entry into the product.
Additional 0.2 µm filter in filtration process
Provides an additional barrier downstream of the existing 0.5 µm filter, covering particulates from process lines, filter components, O-rings and other contact parts.
Additional 0.1 µm filter in nitrogen distribution line
Provides point-of-use filtration of nitrogen used for equipment purging, minimising particulate ingress from the nitrogen distribution system and process lines.